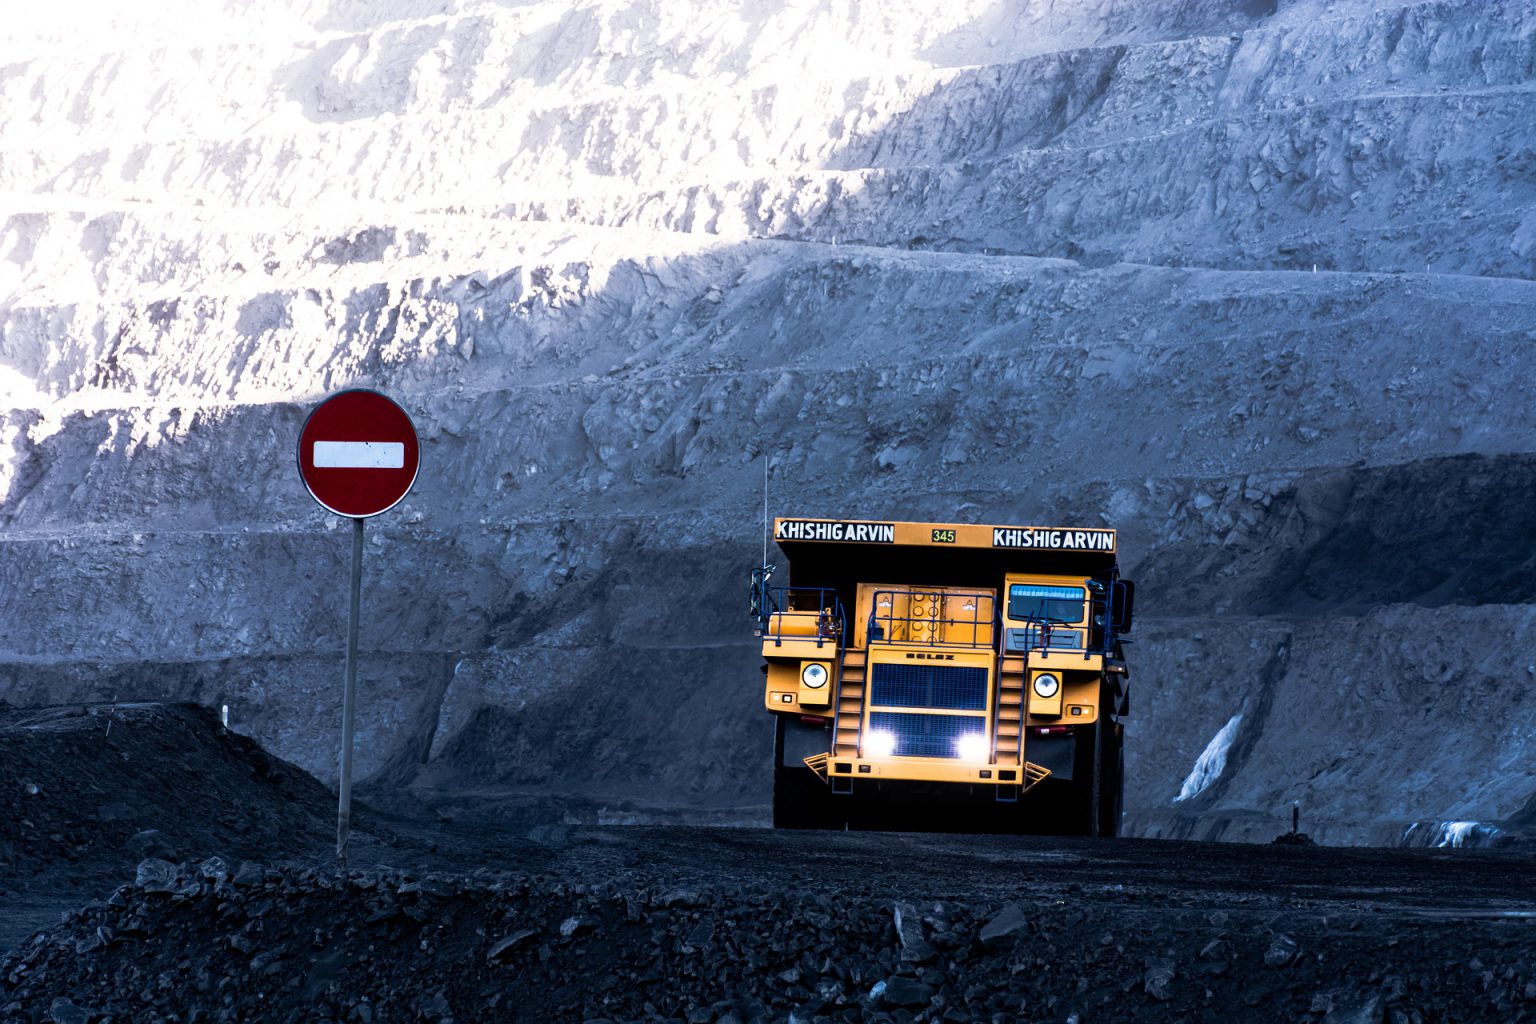
Titan Global Wheel has completed delivery of 220 heavy-load 51-inch rims to two Tier-1 platinum operations in the Bushveld Complex. The rims are designed for 63-inch ultra-class haul trucks running at peak payload, where a rim failure can cost a mine upwards of R2.4 million per shift in lost production.
Order at a glance
Order specification
What changed in the design
The 51″ mining rim programme was a clean-sheet design for Titan. The brief from the operators was specific: lift the load rating by 12%, drop the unfilled rim weight by 6%, and reduce the time-to-fit on a shop floor by half. The team's response was a redesigned spoke geometry, a new hot-rolled steel specification, and a captive-groove bead seat that speeds up tyre mounting.
Pre-production prototypes were tested for 4,200 hours on a dynamometer rig at our Brits facility and across 11 months of in-pit operation at a partner site before commercial release.
Why it matters
A single rim failure on a 800-tonne haul truck can take a production line down for 8 to 14 hours while a recovery crew and replacement rim are mobilised. The direct cost of the lost production dwarfs the cost of the rim itself by a factor of a hundred. Designing for the worst case — a rim that outlasts the tyre, the haul road, and the operator's shift — is what mining fleet owners actually buy.
For mining fleet enquiries, contact our heavy-load team at mining@titanglobalwheel.co.za.